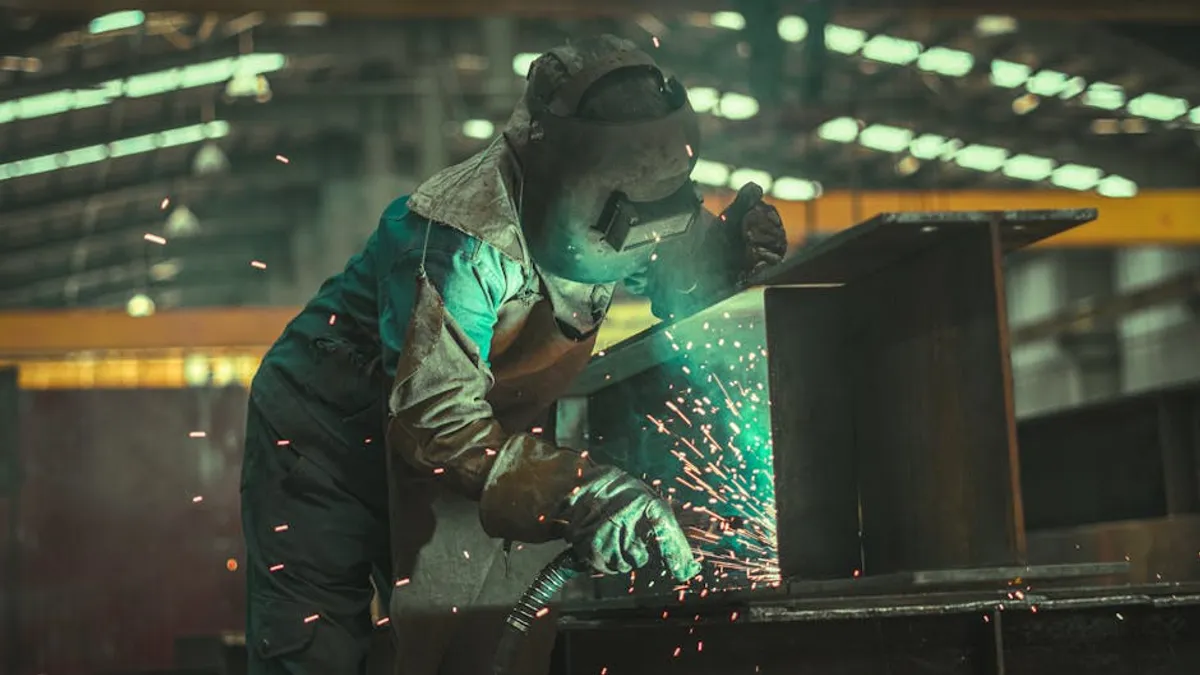
Selecting the appropriate welding process is a foundational decision impacting project cost, structural integrity, and production efficiency. Each welding method presents a unique balance of material compatibility, required skill, equipment investment, and resulting weld characteristics. Understanding these distinctions is critical for engineers, fabricators, and project managers aiming to achieve specific performance requirements while managing budget and timelines. This guide outlines the primary welding types, detailing their operational principles, typical applications, critical specifications, and key considerations for their selection and implementation. This guide outlines the primary welding types, detailing their operational principles, typical applications, critical specificat and offering buying tips to help you choose the right equipment for your needs.
Understanding Core Welding Processes
Shielded Metal Arc Welding (SMAW / Stick Welding)
SMAW, commonly known as stick welding, employs a consumable electrode coated with flux to carry the electric current. The flux disintegrates during welding, creating a shielding gas and slag that protect the weld pool from atmospheric contamination. This process is recognized for its simplicity and versatility.
- Uses: Widely applied in heavy fabrication, construction (structural steel), repair work, and outdoor applications due to its wind resistance. Effective on carbon steels, low-alloy steels, and some stainless steels.
- Specs/Characteristics:
- Equipment: Relatively low initial cost, portable, requires only an electrode holder, ground clamp, power source, and electrodes.
- Skill Level: Moderate to high, requires practice to manage arc length and electrode angle.
- Weld Quality: Produces robust, strong welds, though appearance can be rougher than other methods, requiring post-weld cleaning to remove slag.
- Penetration: Excellent penetration, suitable for thick materials.
- Selection Considerations: Ideal for field repairs or projects where portability is paramount and aesthetic finish is secondary. Less suitable for thin materials or high-volume, precision work.
Gas Metal Arc Welding (GMAW / MIG Welding)
MIG welding utilizes a continuously fed wire electrode that is melted and deposited into the weld joint, protected by an inert or semi-inert shielding gas (typically argon, CO2, or a mix). This process is known for its speed and relative ease of use.
- Uses: Common in automotive manufacturing, sheet metal fabrication, robotic welding, and general fabrication. Excels with carbon steel, stainless steel, and aluminum.
- Specs/Characteristics:
- Equipment: Moderate cost, requires a wire feeder, shielding gas cylinder, welding gun, and power source.
- Skill Level: Relatively easy to learn, making it popular for beginners and high-production environments.
- Weld Quality: Produces clean, smooth welds with minimal spatter, often requiring less post-weld cleanup.
- Speed: High deposition rates, leading to faster welding times.
- Selection Considerations: Favored for production environments requiring high speed and good aesthetic quality. Less suitable for outdoor work without wind protection for the shielding gas.
Gas Tungsten Arc Welding (GTAW / TIG Welding)
TIG welding employs a non-consumable tungsten electrode to create the arc, with a separate filler rod manually fed into the weld pool. An inert shielding gas (usually argon) protects the weld area. This method is praised for its precision and high-quality welds.
- Uses: Critical for aerospace components, medical devices, bicycle frames, and any application demanding high-purity, precise welds. Excellent for stainless steel, aluminum, and exotic metals like titanium and magnesium.
- Specs/Characteristics:
- Equipment: Higher initial cost, requires a TIG torch, foot pedal or finger control, shielding gas, and power source.
- Skill Level: High, requires significant coordination and practice.
- Weld Quality: Produces exceptionally clean, strong, and aesthetically superior welds, often requiring no post-weld finishing.
- Control: Offers precise control over heat input and filler material.
- Selection Considerations: The preferred choice when weld appearance, integrity, and control over heat input are paramount, especially on thin materials or dissimilar metals. Slower process compared to MIG or FCAW.
Flux-Cored Arc Welding (FCAW)
FCAW uses a continuously fed tubular wire electrode filled with flux. This flux provides shielding gas and slag protection, similar to SMAW, but with the continuous feed of MIG. Some FCAW processes also use external shielding gas for enhanced protection (dual shield).
- Uses: Common in heavy equipment repair, shipbuilding, structural steel fabrication, and applications requiring high deposition rates. Effective on thick materials and in outdoor conditions.
- Specs/Characteristics:
- Equipment: Similar to MIG, but uses flux-cored wire.
- Skill Level: Moderate, easier to learn than SMAW but less forgiving than MIG.
- Weld Quality: Produces robust, deep-penetrating welds, often with a rougher appearance and slag to remove.
- Portability: Gasless FCAW is very portable, making it suitable for field work.
- Selection Considerations: An excellent choice for welding thicker materials in outdoor or windy conditions where traditional MIG shielding gas would be compromised. Offers higher deposition rates than SMAW.
Submerged Arc Welding (SAW)
SAW involves an arc submerged under a blanket of granular flux, which protects the weld pool from contamination. A continuously fed wire electrode is used, and the flux melts to form a protective slag layer.
- Uses: Primarily used in automated or semi-automated heavy fabrication, such as pressure vessels, pipelines, structural beams, and large diameter pipes.
- Specs/Characteristics:
- Equipment: High cost, typically large, automated systems.
- Skill Level: Requires skilled operators for setup and monitoring, but less manual skill during the actual weld.
- Weld Quality: Produces extremely high-quality, deep-penetrating welds with excellent mechanical properties and smooth appearance.
- Efficiency: Very high deposition rates, ideal for long, continuous welds on thick materials.
- Selection Considerations: Best suited for high-volume, repetitive welding tasks on thick sections where automation and consistent high quality are critical. Not suitable for small or intricate work.
Resistance Welding (Spot and Seam Welding)
Resistance welding processes join metals by applying pressure and passing a high electric current through the workpieces, generating heat at the interface. No filler material or shielding gas is typically used.
- Uses: Dominant in the automotive industry for joining sheet metal (spot welding), and in manufacturing for fuel tanks, radiators, and appliance components (seam welding).
- Specs/Characteristics:
- Equipment: High initial cost for specialized machinery.
- Skill Level: Low manual skill required during operation, but high setup and maintenance expertise.
- Weld Quality: Produces strong, localized welds without affecting the surrounding material significantly.
- Speed: Extremely fast, highly automated for mass production.
- Selection Considerations: Ideal for high-volume production of thin sheet metal assemblies where speed, consistency, and minimal distortion are priorities. Limited to specific joint designs.
Plasma Arc Welding (PAW)
PAW uses a constricted plasma arc to create a highly focused and intense heat source. This allows for deep penetration and high welding speeds, often on thinner materials than traditional arc welding.
- Uses: Precision welding in aerospace, instrumentation, and medical industries. Effective on stainless steel, titanium, and nickel alloys, often used for keyhole welding on thicker sections.
- Specs/Characteristics:
- Equipment: High cost, requires specialized plasma torch and power source.
- Skill Level: High, similar to TIG but with even more critical setup parameters.
- Weld Quality: Produces extremely narrow, deep, and high-quality welds with minimal heat-affected zone and distortion.
- Speed: Faster than TIG, especially on thinner materials.
- Selection Considerations: Chosen for applications requiring extremely precise, high-speed welds on thin to medium-thickness materials, or for keyhole welding on thicker sections where deep penetration and minimal distortion are crucial.
Pro Tip: Always consider the base material's thickness, composition, and joint configuration before finalizing a welding process. Matching the weld type to these material properties prevents defects, ensures structural integrity, and optimizes material usage.
Selecting the Right Weld Type for Your Project
The optimal welding process is rarely a one-size-fits-all solution. Project demands dictate the choice. For structural components requiring robust, deep welds and field portability, SMAW or gasless FCAW often prove most effective. When speed and good aesthetics on common metals are prioritized in a controlled environment, GMAW is usually the go-to. Precision, aesthetic finish, and material purity on exotic or thin metals point towards GTAW or PAW. Large-scale, automated production on thick materials typically benefits from SAW or resistance welding.
Essential Considerations for Welding Equipment and Materials
Beyond the process itself, the specific equipment and consumables play a significant role. Power source type (AC/DC, constant current/constant voltage), wire feeder capabilities, shielding gas composition, and electrode/filler wire specifications all influence weld quality and production rates. For instance, selecting the correct filler metal alloy is crucial for matching the mechanical properties and corrosion resistance of the base material. Equipment maintenance, calibration, and consumable storage also directly impact performance and safety.
Maximizing Weld Quality and Efficiency
Achieving consistent, high-quality welds and efficient production requires careful attention to detail. This includes proper joint preparation (cleaning, beveling), accurate fit-up, appropriate welding parameters (current, voltage, travel speed), and post-weld inspection. Training and certification of welders ensure adherence to standards and reduce rework. Implementing quality control measures, such as visual inspection, non-destructive testing (NDT), and destructive testing, validates the integrity of the welded joints against design specifications.
Implementing Your Welding Strategy
Successfully executing a welding project involves more than just selecting a process. It requires a holistic approach encompassing material selection, process optimization, equipment procurement or service selection, and rigorous quality assurance. Prioritize safety protocols, invest in proper training, and establish clear quality benchmarks to ensure project success and long-term reliability of welded components. Regular review of welding procedures and technological advancements can further enhance efficiency and weld performance.
Frequently Asked Questions
What is the easiest welding process to learn for beginners?
MIG welding (GMAW) is generally considered the easiest for beginners due to its continuous wire feed, relatively straightforward setup, and less demanding arc control compared to stick or TIG welding.
Which welding method is best for aluminum?
TIG welding (GTAW) is widely regarded as the best method for welding aluminum, offering superior control, clean welds, and excellent aesthetic results. MIG welding can also be used for aluminum, especially on thicker sections, but requires specific equipment and gas.
Can I weld different types of metals together?
Yes, dissimilar metals can be welded, but it often requires specialized filler materials, specific pre-heating or post-heating procedures, and careful selection of the welding process. TIG welding is frequently used for these challenging applications due to its precise control.
What safety precautions are essential for welding?
Essential safety precautions include wearing appropriate personal protective equipment (welding helmet, flame-resistant clothing, gloves), ensuring adequate ventilation to remove fumes, using fire-resistant screens, and having fire extinguishers readily available. Always follow manufacturer guidelines and safety standards.